Common MIG welding problems include difficult arc starts, unstable arcs or wire burnback, porosity, dirty welds, cracking, insufficient penetration or fusion, overheated supply cables, and uneven wire feed. The most practical first step is to identify the visible symptom, then check the gas path, polarity, wire-feed path, torch, and welding settings in that order.
MIG welding is a semi-automatic process commonly used where long, continuous welds or substantial weld buildup are needed. Because several systems work together during welding, one fault can have more than one possible cause.
Summary: Check shielding gas and connections when the arc is hard to start or welds are contaminated. Inspect drive rolls, contact tube, and liner for unstable arcs or uneven wire feed. Review current, travel speed, arc length, joint preparation, and torch angle for weld-quality defects.
Why is a MIG arc difficult to start?
A hard-to-start MIG arc may be associated with the gas supply being closed or empty, incorrect polarity, poor electrical connections or work clamp contact, or a control-circuit issue. Check the gas valve and cylinder, inspect the work clamp and power connections, and verify the required polarity stated in the source: DCEP, with the electrode positive and workpiece negative.
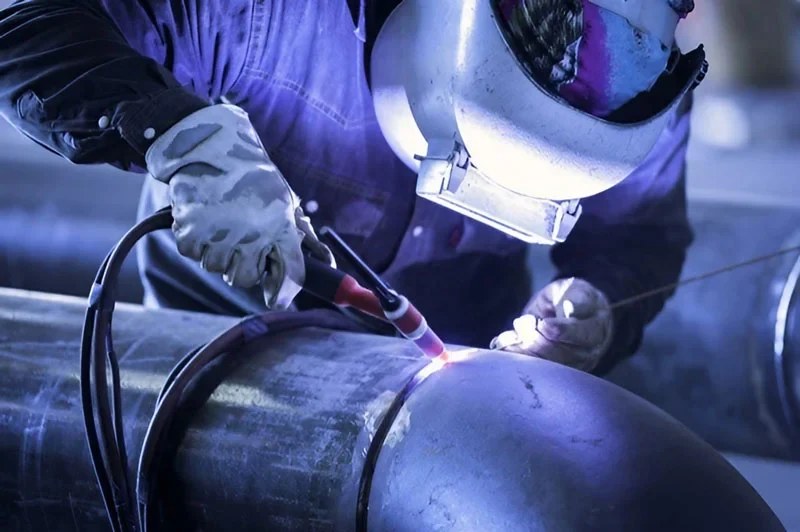
What causes wire burnback and an unstable MIG arc?
Wire burnback or an erratic arc can result from incorrectly sized drive rolls, unsuitable drive-roll pressure, slow wire-feed speed, a worn or contaminated contact tube, unstable input voltage, incorrect polarity, an overheated torch, or a dirty or worn liner. Start by matching the drive-roll size to the wire and adjusting pressure so the wire feeds without slipping or being crushed.
- Increase wire-feed speed if it is too low.
- Clean or replace a worn contact tube and replace a dirty or worn liner.
- Check the power supply and polarity.
- If torch overheating is involved, inspect the torch and its cooling system where applicable.
How can porosity and a dirty MIG weld be corrected?
Porosity can occur when shielding gas flow is disturbed, the gas is damp, the torch leaks, the workpiece carries oil, or excessive spatter affects the weld pool. A dirty weld is likewise linked in the source to insufficient shielding gas.
Adjust gas flow for the nozzle size, inspect the torch for leaks, and clean oil from the workpiece with solvent and a stainless-steel brush. Clean and dry feed components, keep the liner from bending sharply, and adjust welding parameters if excessive spatter or cooling conditions are contributing.
Why do hot cracks or crater cracks form in MIG welds?
Hot short cracks may be linked to an unsuitable wire type, incorrect joint design, unsuitable fixturing, slow travel speed, or welding technique. Check joint gap, root dimensions, bevel angle, wire selection, fixturing, torch angle, and deposition rate before revising the process.
Crater cracks are associated with improper weld termination. The source recommends briefly welding back at the end, finishing with a smaller weld pool, or using runoff tabs at the start and end of the weld.
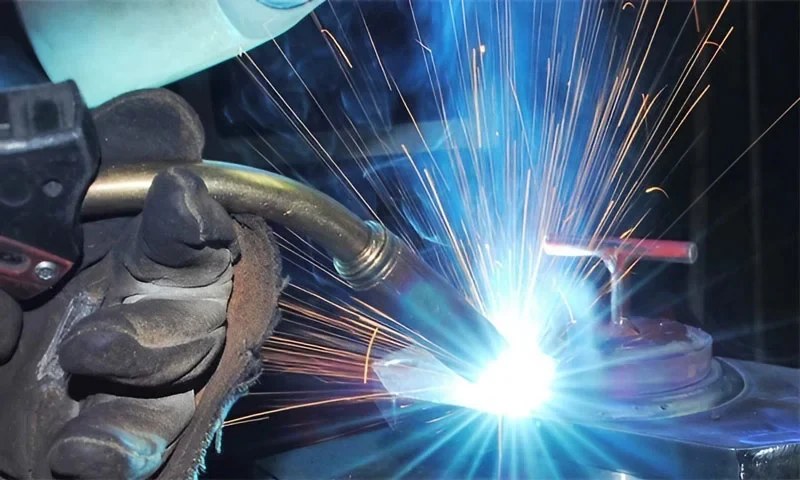
What should be checked when penetration or fusion is insufficient?
Insufficient penetration is associated with excessive travel speed, low welding current, an arc that is too long, or an incorrect welding angle. Reduce travel speed, raise current as appropriate, shorten the arc, and correct the torch angle.
Insufficient fusion is associated with poor joint preparation, excessive arc length, or contamination at the joint. Verify the gap, root dimensions, and bevel angle; shorten the arc; and clean the joint before welding.
| Weld condition | Likely checks | Corrective direction from the source |
|---|---|---|
| Insufficient penetration | Travel speed, current, arc length, torch angle | Slow travel, increase current, shorten the arc, correct angle |
| Insufficient fusion | Joint preparation, arc length, joint cleanliness | Check joint geometry, shorten the arc, clean the joint |
Why does a welding supply cable become too hot?
An overheated welding supply cable may indicate an undersized cable, loose cable connections, excessive cable length, or inadequate cooling. Check that the cable size and length are appropriate, tighten connections, and inspect the cooling circuit for adequate water flow and leaks where water cooling is used.
What should you check if a MIG welder has an inconsistent wire feed ?
An inconsistent wire feed in a MIG welder can be caused by the wire becoming kinked or tangled, an excessively long welding torch, rusted welding wire, improper pressure on the drive rolls, or a worn-out torch liner (conduit liner) that hasn't been replaced. First, ensure the wire path from the spool to the torch is straight, and avoid any sharp bends or kinks when installing the wire.
Use clean, dry welding wire; replace the spool if the wire shows signs of rust.
Adjust the drive roll pressure so that it is sufficient—neither too loose nor too tight.
Avoid bending the welding torch excessively during operation, and ensure the torch length is appropriate for the task.
Clean or replace the torch liner periodically, depending on the frequency of use.
Note: The troubleshooting steps above address specific symptoms. When inspecting control circuits, electrical systems, or cooling systems, always follow proper safety procedures.