Laser welding for aluminum by concentrating energy at a small weld area. This approach is presented as a way to reduce heat spread, which is important because aluminum conducts and reflects heat readily.
For aluminum work, the practical result depends on material thickness, filler wire where needed, laser settings, feed speed, surface preparation, and a trial weld before production.
Summary: Laser welding focuses heat at the aluminum joint. It may use filler wire or weld without it in some cases. The supplied reference settings cover 1–6 mm material thickness. Clean surfaces, stable setup, and operator protection remain essential.
Can a laser welding machine weld aluminum?
Yes. A laser welding machine directs a concentrated laser beam onto the aluminum joint, locally melts the surface, and allows it to cool into a continuous weld. Filler wire may be used or omitted depending on the joint and application.
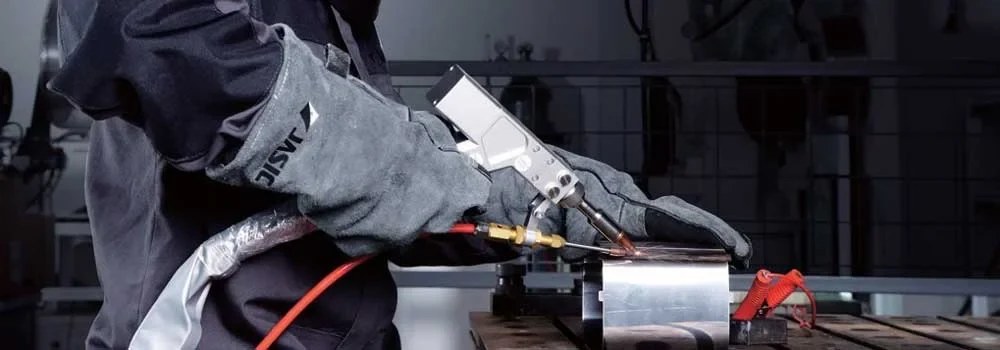
Aluminum can be challenging to weld because it conducts heat and reflects heat strongly. The supplied material also identifies distortion, porosity associated with oxidized surfaces, and burn-through on thin sheet as issues that require careful heat control.
How does laser welding aluminum differ from MIG or TIG welding?
According to the supplied comparison, laser welding applies heat more locally than conventional MIG or TIG processes. This is associated with a smaller heat-affected area and less risk of distortion, especially on thinner aluminum sections.
| Criterion | Laser welding aluminum | Conventional MIG/TIG aluminum welding |
|---|---|---|
| Heat effect | Concentrated at the weld point | Heat spreads more widely |
| Distortion | Intended to limit warping | More prone to warping, particularly on thin material |
| Weld finish | Described as small, smooth, and bright | May require grinding or polishing after welding |
| Filler material | May be unnecessary for some joints | Uses welding wire and shielding gas |
| Speed | Listed as 3–5 times faster | Listed as slower and more dependent on operator skill |
Note: The stated 3–5 times speed comparison is a general reference from the supplied material. Actual results should be verified on the intended aluminum part and joint design.
Which settings matter when laser welding aluminum?
The key variables are aluminum thickness, filler-wire diameter when wire is used, laser setting in watts, weld-bead width, and filler-wire feed speed. These settings should be coordinated because excessive input can burn through thin material, while unsuitable wire feed can leave a joint underfilled or overly raised.
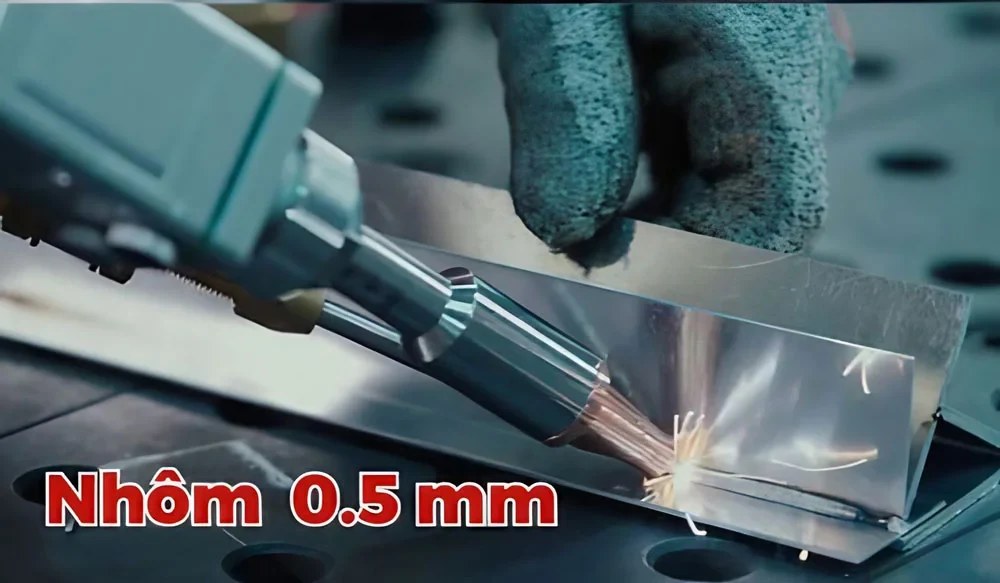
| Aluminum thickness (mm) | Filler wire diameter (mm) | Laser setting (W) | Weld bead width (mm) | Wire feed speed (cm/min) |
|---|---|---|---|---|
| 1 | 1 or 1.2 | 700–900 | 2.5 ± 0.5 | 50–70 |
| 1.5 | 1 or 1.2 | 750–950 | 2.5 ± 0.5 | 50–70 |
| 2 | 1 or 1.2 | 800–1000 | 2.5 ± 0.5 | 50–70 |
| 2.5 | 1 or 1.2 | 800–1100 | 2.5 ± 0.5 | 50–70 |
| 3 | 1 or 1.2 | 1000–1300 | 2.5 ± 0.5 | 50–70 |
| 4 | 1 or 1.2 | 1000–1500 | 2.5 ± 0.5 | 50–70 |
| 5–6 | 1.2 | 1000–1500 | 2.5 ± 0.5 | 50–70 |
These figures are reference values supplied for aluminum alloy welding, not universal machine settings. A sample weld is recommended before volume production to check weld appearance and consistency.
Where can laser welding aluminum be applied?
The supplied material identifies aluminum laser welding for mechanical fabrication, construction and interiors, signage and display work, electrical and electronic enclosures, and vehicle-related components. Examples include frames, brackets, machine housings, doors, railings, display frames, LED housings, and aluminum pipes.
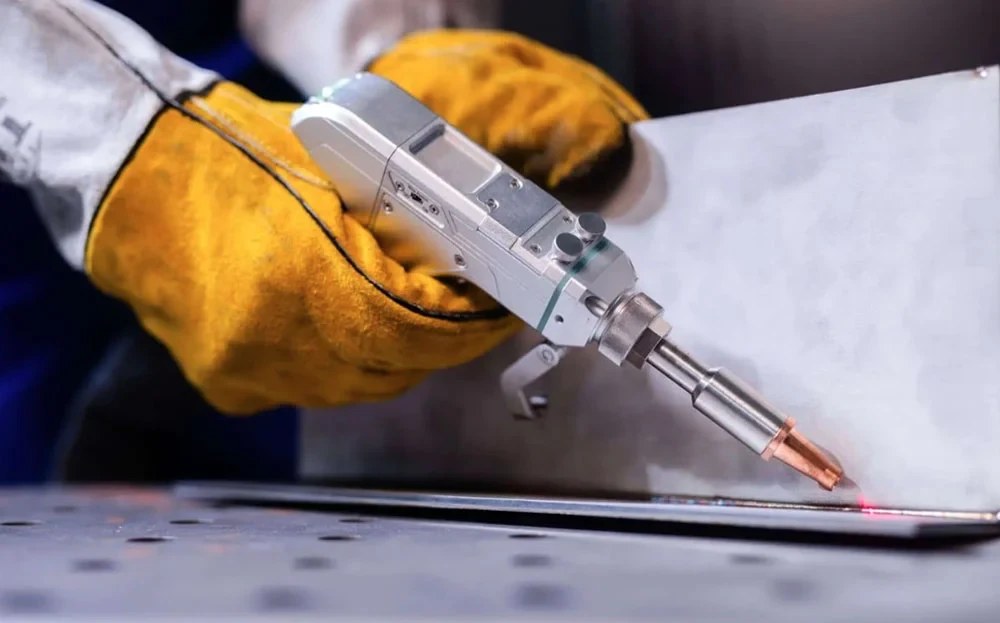
For production environments, the material also notes that laser welding can be integrated with robots or CNC equipment. Whether that integration is appropriate depends on the specific production process and equipment setup.
What preparation and safety steps are important for aluminum laser welding?
Clean the aluminum surface before welding to remove oxide layers, then set the laser input and wire feed for the material thickness. Maintain a steady wire feed and make a test weld before repeating the operation across a production batch.
- Use a clean, ventilated work area and avoid direct sunlight at the welding location.
- Do not direct a fan at the weld area, as it may disturb shielding gas and contribute to porosity.
- Keep combustible materials such as paper, plastic, and chemicals away from the machine; the supplied guidance specifies at least 5 m.
- Use the shielding gas specified for the process, identified in the supplied material as argon or nitrogen.
- Wear laser welding eyewear, gloves, and protective clothing; never look directly at the laser beam.
- Have experienced technicians perform maintenance or repairs and follow the manufacturer’s electrical instructions.
When should filler wire be used for laser welding aluminum?
Filler wire is not required for every laser welding machine, but the supplied material describes it as useful for adding material to the joint. It is particularly relevant for thicker aluminum or where a fully filled, sealed weld is required.
For the listed settings, 1.2 mm filler wire is used for 5–6 mm aluminum. The material advises choosing wire diameter to suit thickness and keeping feed speed stable so the bead does not become incomplete or uneven.