How Plastic Surface Gloss Affects Perceived Color Saturation & How to Measure It Correctly
Decoding the optical phenomena of specular reflection and diffuse reflection, differentiating between SCI and SCE measurement modes, and guiding the combined use of colorimeters and gloss meters to accurately separate color shade errors from surface gloss defects.
1. Why Do Glossy Parts Look Darker Than Textured Parts of the Same Color?
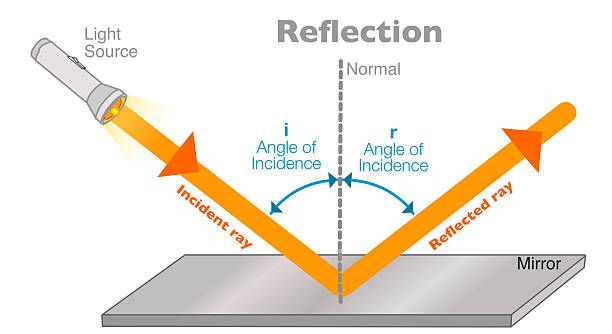
Light incident on a plastic surface reflects through two distinct optical mechanisms. Specular Reflection is the component of light that bounces off in a single direction at an angle equal to the angle of incidence (like a mirror). Diffuse Reflection is the light that penetrates the plastic layer, interacts with pigment particles, and scatters in all directions. The actual perceived color of an object is primarily determined by this diffuse reflection component.
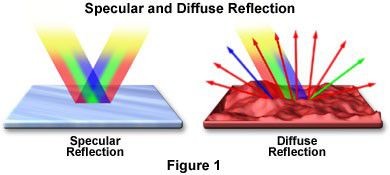
Glossy surfaces exhibit strong specular reflection, concentrating the reflected beam into a specific direction. An observer viewing from other angles receives mostly diffuse light carrying the pigment color, making the part appear darker, richer, and more saturated. Conversely, a textured or matte surface scatters specular white light in many directions. More unabsorbed white light reaches the observer's eyes simultaneously, causing the color to look lighter, paler, and less saturated.
| Optical Characteristics | Glossy Surface (High Gloss) | Matte / Textured Surface |
|---|---|---|
| Dominant Reflection Mode | Specular reflection, concentrated in a single direction. | Diffuse reflection, scattering light in all directions. |
| Surface White Light Behavior | Reflects away from the observer's line of sight at standard viewing angles. | Mixes directly with diffuse colored light entering the observer's eye. |
| Visual Perception | Color appears darker, richer, deeper, and more saturated. | Color appears lighter, paler, brighter, and less saturated. |
2. Surface Gloss Levels (GU Scale) & Human Visual Perception
The Gloss Unit (GU) scale categorizes perceived color saturation levels according to surface quality control standards:
Specular reflection reflects away from the viewing angle, allowing color to achieve peak depth and true pigment saturation.
A portion of white light begins to scatter, slightly reducing color saturation compared to high-gloss samples.
Strong diffuse scattering overpowers pigment reflection, making the color appear noticeably lighter and paler to the naked eye.
Key takeaways for QC personnel: Two parts manufactured with the exact same color masterbatch formula but differing surface gloss will be perceived as a color mismatch by the human eye. QC teams must separate pigment errors from surface gloss variations, as their root-cause adjustments on the injection molding machine are fundamentally different.
3. What Causes Surface Gloss Variations in Injection Molded Parts?
Plastic surface gloss can fluctuate due to 4 primary technical factors in the molding shop:
- Mold Cavity Surface Finish: Mirror-polished molds yield high gloss, textured molds (e.g., VDI / Mold-Tech grain) produce matte finishes, and gradual mold wear changes surface gloss over time.
- Injection Molding Parameters: High mold temperatures, higher hold pressures, and fast injection speeds help the melt replicate the cavity finish more accurately (higher gloss). Contact with cooler mold walls results in a duller finish.
- Resin & Additives: Base polymer selection (ABS, PC, PP) and filler content (glass fiber, talc) significantly reduce surface gloss.
- Post-Molding Operations: Secondary processes such as spray coating, pad printing, or matte/gloss film lamination.
4. How to Measure Color Without Being Fooled by Gloss: Choosing SCI vs. SCE
Integrating sphere spectrophotometers (d/8 geometry) allow measurement in 2 distinct specular reflection handling modes:
Includes specular reflection in the measurement data. Captures true pigment color independent of surface gloss or texture finish.
Excludes specular reflection from the measurement data. Correlates directly with visual human perception (glossy samples measure darker than matte samples of the same color).
QC Data Analysis Rule:
- If Delta E in SCI is low but Delta E in SCE is high: The perceived color difference is caused entirely by surface texture or gloss variations, while the pigment formulation is compliant.
- If Delta E in both SCI and SCE is high: True color deviation has occurred, requiring adjustments to masterbatch ratio, barrel temperatures, or raw material supply.