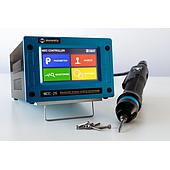
RPM can affect the torque outcome when an electric torque screwdriver fastens an assembly joint. The effect depends on joint conditions and the forces involved, so a validated RPM setting should be documented and kept consistent.
Residual torque checks help confirm that adequate torque reached the fastener after assembly. They can also help identify missed or loose fasteners and potential joint relaxation.
Summary: RPM may contribute to the torque applied to a joint. Higher and lower RPM change the duration of applied force and may change inertia. Use a consistent, documented speed after validation. Check residual torque with a method suited to the joint.
Does RPM affect the torque applied to a fastened joint?
Yes, RPM settings can contribute to the torque applied to a joint. RPM is one of several assembly variables, alongside joint hardness, material, and whether a screw is lubricated or has a locking patch.
The size of the RPM-related difference is not fixed. In some applications it may be insignificant, while in others it may be more pronounced; the joint should therefore be checked rather than judged by speed alone.
What is the difference between higher and lower RPM for torque assembly?
Higher RPM applies force for a shorter time, while lower RPM applies force for a longer time. The source describes this as less energy applied at higher RPM and more energy applied at lower RPM.
| RPM setting | Force duration and energy described | Potential inertia effect |
|---|---|---|
| Higher RPM | Force is present for less time, with less energy applied to the joint. | May increase inertia. |
| Lower RPM | Force is present for more time, with more energy applied to the joint. | May result in less inertia. |
Inertia-related differences depend on the mass of the force generated. For that reason, neither a higher nor lower RPM setting can be treated as a universal torque correction for every joint.
Why should a validated RPM setting remain unchanged?
A validated RPM setting should remain unchanged because consistent speed supports calibration validation and correlation. Changing RPM after validation can introduce a variable into the fastening process and make prior results less directly comparable.
A formal setting and validation plan should record the RPM used for the application. It should also include residual torque checking at the joints, since the final joint condition is the relevant result to verify.
What is residual torque in a threaded fastener joint?
Residual torque is the tension that remains in a joint after a threaded fastener has been tightened. Checking it after assembly helps verify that adequate torque was delivered to the fastener.
A residual torque check may detect a missed fastener, a loose fastener, or joint relaxation. Friction differs between rundown and static conditions, however, and this difference must be considered when engineering a residual torque specification.
Note: A post-assembly torque reading is not automatically identical to the torque present during rundown. Static and rundown friction can differ, so the verification approach should be defined for the joint being evaluated.
Which methods can verify torque at an assembled joint?
Three described methods are the first movement test, the loosening test, and the marking test. Each uses movement of the fastener to establish a torque reading or reference, but they do not provide the same type of result.
| Verification method | How it is performed | Result described |
|---|---|---|
| First movement test | Slowly apply force with a torque measuring tool until the fastener first moves. | Indicates the original torque applied and is described as the best way to determine residual torque. |
| Loosening test | Apply torque in the loosening direction until the fastener breaks loose. | Provides an approximate indication of torque applied to the joint. |
| Marking test | Mark the tightened assembly, loosen it, then retighten until the marks align. | The torque needed to return to the original location is a reference for the original applied torque. |
Why is torque verification important after fastening?
Torque verification checks whether the product was fastened correctly and supports quality, safety, and reliability objectives. An insufficiently tightened fastener may vibrate loose, while excessive torque can strip a threaded fastener.
The check should follow an established torque specification and a consistent validation plan. The source identifies dial screwdrivers, dial wrenches, and torque testers with a Rotary Torque Sensor or Torque Screwdriver Sensor as equipment used to move the fastener during these tests.
What is a practical approach to RPM and torque control?
Start with the joint-specific torque specification, then validate and document the RPM setting used to reach it. Keep that setting consistent after validation and check residual torque on the joint rather than assuming a speed change has no effect.
This approach accounts for variables that can influence the fastening outcome, including joint hardness, material, lubrication, locking patches, force duration, inertia, and friction differences between rundown and static conditions.