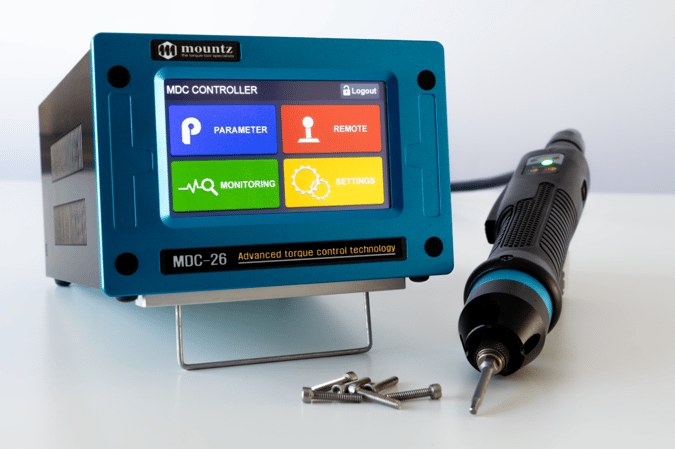
Electronics manufacturing torque tools help control fastening work by applying defined torque requirements and supporting process documentation. In the supplied example, DC-controlled tools are used to manage torque, fastening sequences, tolerances, bit selection, and assembly-line data.
For electronic assemblies, a fastening deviation can contribute to faults or device malfunction. A controlled tool system therefore supports a more repeatable process than relying only on an operator to remember the required torque, sequence, and bit.
Summary: Controlled DC tools can apply repeatable torque. Programmable controllers can enforce fastening sequences and tolerances. A linked bit tray can prevent operation when the wrong bit is selected. Assembly data can show time spent at a station and on each fastener.
Why does torque control matter in electronics assembly?
Torque control matters because each screw or fastener must meet the applicable assembly specification, and its result may need to be recorded. The source material identifies incomplete fastening and use of an incorrect bit as process risks when compliance and reporting depend on individual operators.
Repeatable torque control is particularly relevant where circuit boards, hard drives, and other electronic components require consistent assembly work. The goal is not simply to tighten a fastener, but to perform the required fastening operation in a controlled, documented manner.
How do MD-Series DC control tools support a fastening process?
According to the supplied material, MD-Series DC control tools are designed to achieve accurate, repeatable torque control for each tightened fastener. Their controller can be programmed with fastening sequences and torque tolerances for the assembly operation.
This arrangement can act as a control point at an assembly station: an assembly is not cleared until the specified requirements are met. It shifts key checks from memory-based work toward controller-defined requirements.
| Process need | Control described in the source |
|---|---|
| Torque requirement | Repeatable torque control for each fastener |
| Fastening order | Programmable fastening sequences |
| Acceptance range | Programmable torque tolerances |
| Assembly release | Controller-based confirmation before clearing an assembly |
How can a tool system help prevent incorrect bit selection?
The described solution links a customized bit socket tray directly to an MDC controller. Sensors in the tray detect different colors of tape wrapped around individual bits, while a barcode on the board identifies the bit the operator should remove.
If the operator chooses the wrong bit or does not attach it correctly, the DC assembly tool does not activate in the example provided. This interlock is intended to stop the fastening step before an incorrect tool selection becomes an assembly error.
What production data can controlled fastening tools capture?
The source states that the power-tool solution can capture data throughout the assembly line. Examples include the time a circuit board spends at a station and the time taken to fasten each fastener.
These data points can help a manufacturer examine how work moves through the line and inform future assembly-line design decisions. They also provide process information beyond a simple pass or fail result for the fastening action.
| Captured item | Potential process use stated in the source |
|---|---|
| Time at each station | Review assembly-line flow and efficiency |
| Time to fasten each fastener | Examine fastening activity within the process |
| Fastening compliance | Support adherence to assembly specifications |
When should an electronics manufacturer consider a controlled fastening workflow?
A controlled workflow is relevant when an assembly requires defined torque, a specified fastening sequence, documented results, or a particular bit for a given board. It is also relevant when the process needs to reduce the opportunity for incomplete fastening or incorrect bit use caused by distraction.
The appropriate setup depends on the application requirements and the documented assembly specification. The supplied material supports evaluating the torque requirement, tolerance, sequence, bit-selection method, and process data needed at each station.
What should be defined before configuring a torque-controlled assembly station?
Before configuration, the manufacturer should have comprehensive documentation for the fasteners and assembly steps. This includes the required torque for each screw or fastener, the sequence to follow, the applicable tolerance, and whether the result must be recorded.
Where several bits are used, the source example also shows the value of defining the correct bit for each board and connecting that selection to the fastening process. Clear requirements give the controller and operator a consistent basis for performing the task.