Offset printing blanket thickness gauge is an important part of maintaining stable image transfer and consistent print quality. In an offset press, the inked image moves from a metal plate cylinder to a rubber blanket cylinder before reaching the printing surface. The contact condition between these cylinders depends on the combined thickness of the blanket and its packing material.
Because blankets and packing are repeatedly compressed during production, their thickness can gradually change. Periodic measurement helps operators monitor this change, maintain the intended cylinder contact, and make better-informed maintenance decisions.
Why blanket thickness matters in offset printing
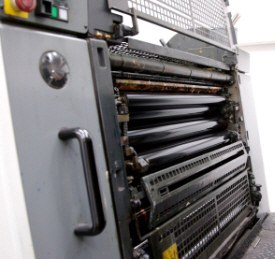
Efficient image transfer requires controlled pressure, often called squeeze, where the plate and blanket cylinders meet. Packing material, such as paper or fiber, is placed beneath the rubber blanket so that the blanket extends slightly beyond the cylinder surface. This creates the overlap needed for the cylinders to press against one another at the contact point.
The source material describes a typical squeeze range of 0.004 to 0.006 in. (4–6 mils, or 0.1–0.2 mm). This dimension is closely tied to print quality. Insufficient squeeze can reduce image-transfer effectiveness, while excessive squeeze can contribute to dot slur or smearing.
Measuring blanket thickness alone is therefore not the full picture. Operators should also consider the packing and plate materials when assessing the dimensional condition of an offset press.
What changes during press operation
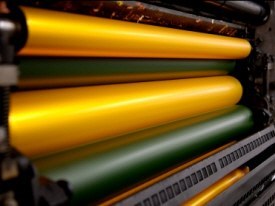
Printing blankets and the packing beneath them are under continual compression. Over time, this may reduce the thickness of both layers and alter the squeeze condition. Monitoring thickness at regular intervals provides a way to observe compression and wear rather than relying only on visible print defects.
Blanket service life can vary with the press type and the nature of the work being printed. The provided information notes that rubber blankets generally last from three to six months. Regular thickness checks can support decisions about when a blanket may need replacement, while also helping maintain more repeatable conditions between print runs.
Limitations of needle-based measurements
Traditional analog needle instruments can measure blanket and packing thickness on the press by penetrating the blanket and contacting the metal cylinder below the packing. While this method provides a measurement approach, puncturing the blanket can damage its surface.
The puncture holes may also allow chemical solvents to reach the packing material. If localized swelling occurs beneath the blanket, the resulting dimensional variation can affect image quality and may contribute to smearing. For applications where preserving blanket integrity is important, a non-destructive approach can be preferable.
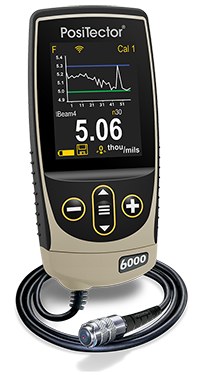
Using PosiTector 6000 for thickness checks
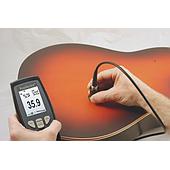
The PosiTector 6000 coating thickness gage is identified in the source material as a handheld option for measuring blanket, packing, and plate thickness on an offset press. It uses magnetic or eddy current measurement principles rather than piercing the blanket, allowing measurements to be taken without leaving puncture holes.
This approach can be used across the cylinder width, enabling repeated checks at different locations. The instrument's built-in statistics function can update and display average readings across the measured surface. Its memory and downloading capabilities can also help an operator record changes in blanket and packing compression over time and across different print operations.
Probe selection by cylinder material
For blanket, packing, and plate measurements on a steel press cylinder, the source specifies the PosiTector 6000 FTS probe. Where the press cylinder is stainless steel or aluminum, it specifies the FNTS probe. Selecting the probe based on cylinder material is essential to the stated measurement application.
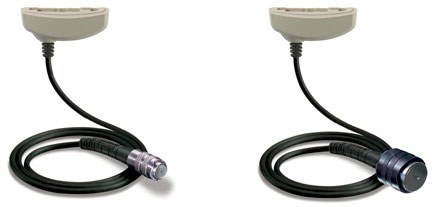
According to the provided data, these interchangeable probes measure thicknesses from 0 to 250 mil (6 mm), with a maximum accuracy of ±0.5 mil (0.01 mm) + 1% of reading. Microprobes are also available for applications with hard-to-reach measurement areas.
Building a useful measurement routine
A consistent routine can make offset printing blanket thickness measurement more valuable. Measure comparable locations across the cylinder, record blanket and packing readings, and compare trends over time. When the measured thickness changes, review the squeeze condition alongside print results and normal maintenance observations.
By tracking these dimensions, operators can better understand how compression and wear develop during production. This supports a more controlled approach to maintaining blanket condition, packing setup, and the print quality expected from the press.
The coating thickness gauge not only helps consistently monitor and evaluate the condition of offset printing blankets but also provides operators with clearer data on the material layers that determine contact pressure within the printing system.