A powder coating thickness gauge is a specialized instrument used to measure the thickness of powder coating on metal or non-metal surfaces, helping ensure coating quality and durability while minimizing material consumption.
This is an important quality control step in metalworking, metal structure manufacturing, and surface finishing. The coating must meet the specified thickness range to provide adequate protection, maintain the desired appearance, and ensure compatibility during part assembly. The appropriate measurement method depends mainly on the substrate material, whether the powder coating is uncured or cured, the geometry of the part, and data storage requirements for inspection.
Why measure powder coating thickness?
Too little powder may provide insufficient coverage and protection. On metal parts, inadequate thickness can reduce protection against environmental effects such as corrosion on steel or oxidation on aluminum. It can also contribute to an inconsistent surface finish, color, or appearance.
Excessive film thickness can also create problems. It may affect curing efficiency, part fit, adhesion, and the tendency of a coating to peel or chip. Regular inspection provides objective data for adjusting the application process, checking incoming coated components, and documenting quality-control results where required.
Post-cure powder coating thickness measurement
After curing, dry film thickness targets are commonly used for inspection. Handheld instruments can provide non-destructive measurements using magnetic, eddy current, or ultrasonic principles. The correct principle is determined by the substrate.
Steel substrates: magnetic measurement
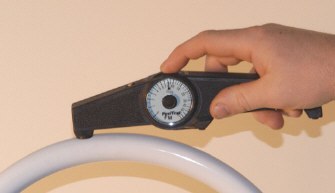
For non-magnetic coatings on steel, magnetic thickness gauges are used. Mechanical pull-off gauges determine thickness from the force needed to remove a permanent magnet from the coated steel surface. These instruments can be suitable for basic checks where only a limited number of readings is needed.
Examples include the PosiTest FM, a dial-type magnetic pull-off gauge, and the PosiPen, a pencil-type gauge with a small probe tip for small parts, curved surfaces, and difficult-to-reach locations.
Electronic gauges provide displayed readings and are used for post-cure measurement on metal components. The PosiTest DFT Ferrous is intended for steel substrates, while the PosiTest DFT Combo is intended for metal substrates. The PosiTector 6000 series includes F series instruments for steel, N series instruments for non-steel materials such as aluminum, and FN series instruments for either application.
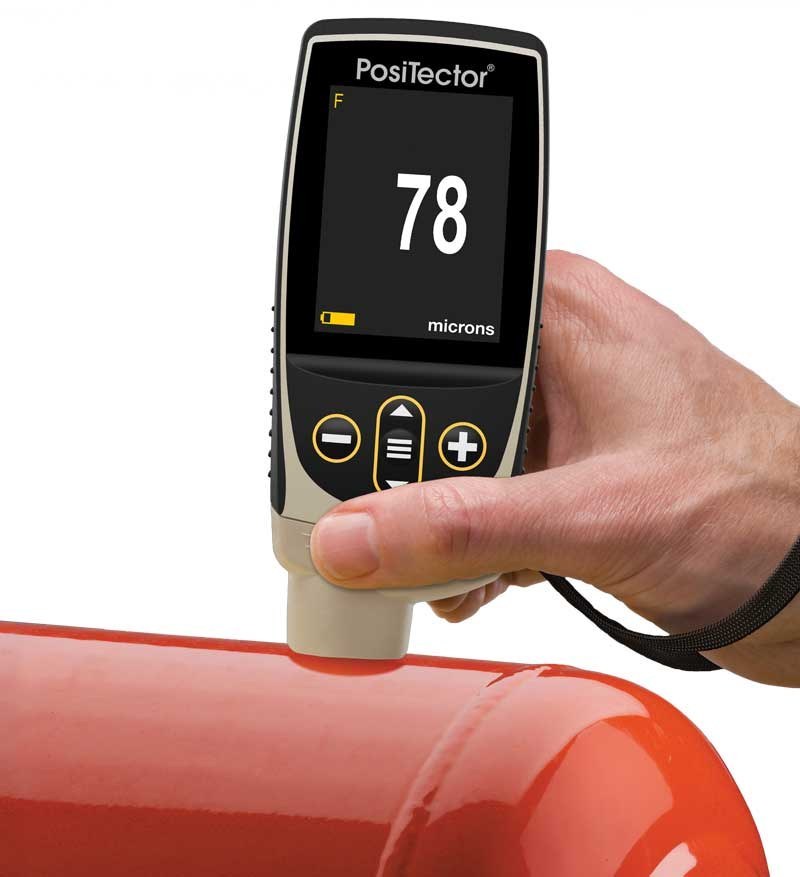
ASTM D7091 describes non-destructive coating thickness measurements over metal substrates using magnetic and eddy current gauges.
Aluminum and other non-ferrous metals: eddy current measurement
When a non-conductive coating is applied to aluminum or another non-ferrous metal, eddy current measurement is the applicable principle described in the source material. A combination gauge or an instrument configured for non-ferrous substrates allows inspectors to measure cured powder coating without damaging the part.
Wood, plastic, and other non-metal substrates: ultrasonic measurement
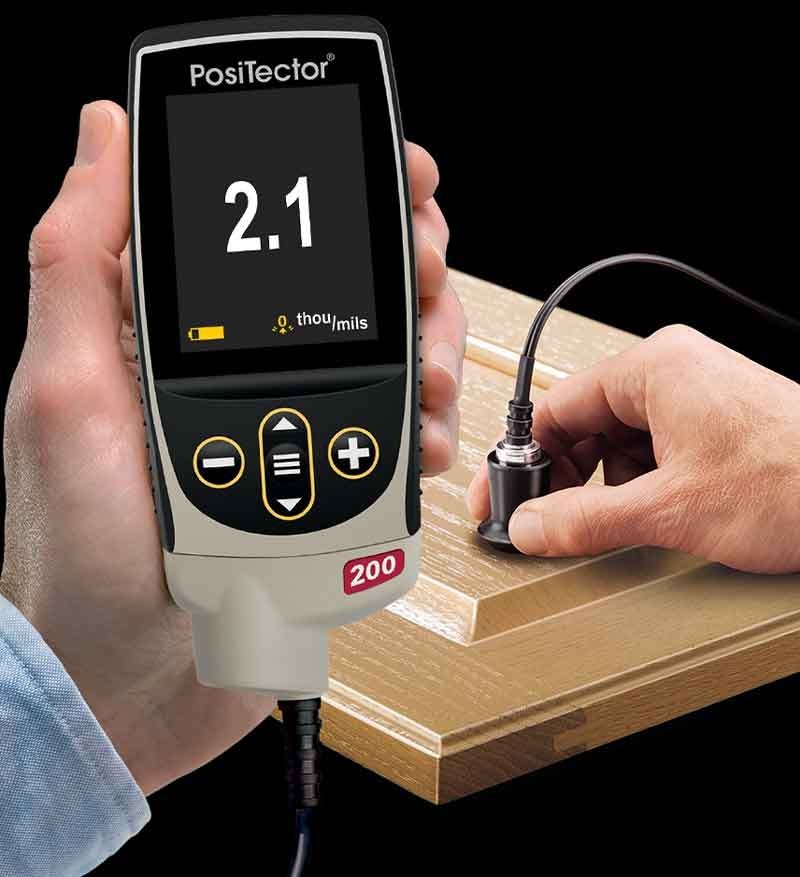
Magnetic and eddy current techniques are intended for metal substrates. Coated wood, plastic, and other non-metal parts require ultrasonic pulse-echo measurement. This method uses a probe with a temporary coupling medium, such as gel or a drop of water, on the coating surface.
An ultrasonic instrument may also distinguish individual layers in a multi-layer coating system. The PosiTector 200 B is identified for measuring powder coating on non-metal substrates. ASTM D6132 describes non-destructive ultrasonic thickness measurement over non-metal substrates.
Alternative post-cure methods
A micrometer can be used with many coating and substrate combinations when the bare substrate is accessible. The thickness is calculated from the difference between a reading on the coated part and a reading without the coating.
Destructive methods include cross-sectioning a coated part for microscopic examination or making a geometric incision through the cured coating for optical measurement. These methods may be used when non-destructive methods are not possible or when confirmation is needed. ASTM D4138 describes destructive cross-section measurements over rigid substrates.
Pre-cure measurement and cured-thickness prediction
Measuring uncured powder helps identify application issues before the curing process is complete. This can be especially useful on moving production lines, where waiting for post-cure measurements may delay corrective action and increase rework or scrap.
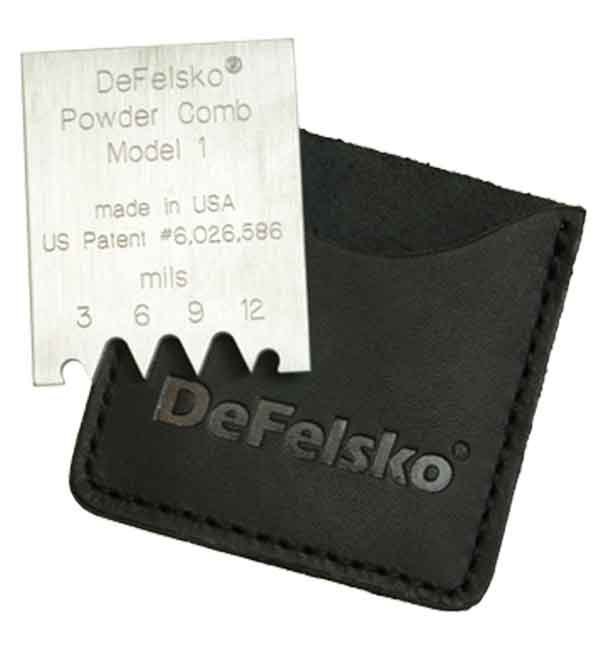
ASTM D7378 describes three approaches for measuring pre-cured powder and predicting cured thickness: notched metal comb gauges, electronic gauges with a special powder probe, and non-contact ultrasonic instruments.
Powder combs and special powder probes
A Powder Comb is drawn through uncured powder to determine a height range from the teeth that contact the coating. A special powder probe can also measure powder height on metal substrates by penetrating the powder to the substrate. Both methods can leave marks in the uncured powder and provide height rather than final cured thickness.
Because powder can diminish in thickness during curing, a reduction factor should be established for the specific powder. This is done by comparing pre-cure and post-cure readings at corresponding locations across different thicknesses.
Non-contact ultrasonic pre-cure inspection
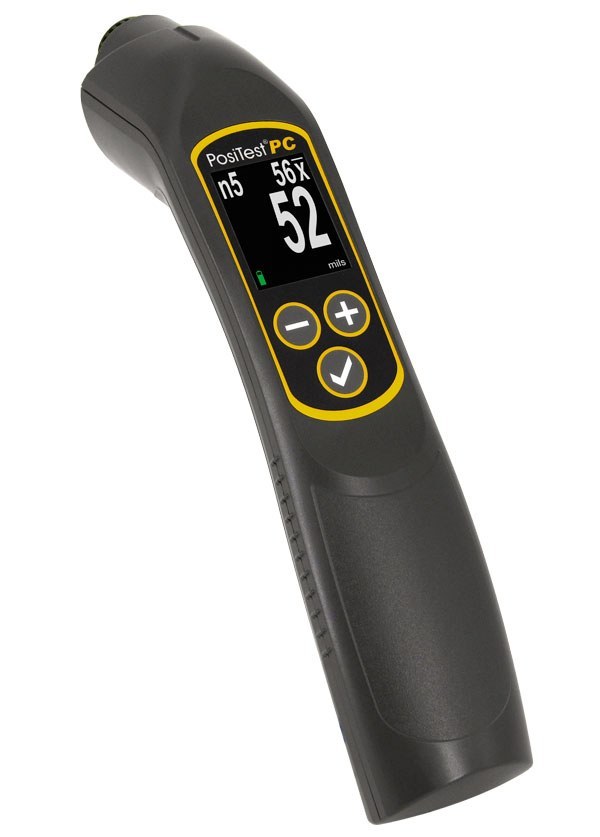
The PosiTest PC Powder Checker is described as a non-contact ultrasonic instrument for uncured powder. Rather than reporting powder height alone, it provides a predicted cured thickness result. Because it does not contact the powder surface, measured components can continue through the process without measurement marks.
Units and inspection planning
If the goal is to make adjustments before curing, choose a solution designed for uncured powder and distinguish between powder height measurement and cured film thickness prediction. The measurement results should then be compared with the requirements specified in the coating material’s technical data sheet and the quality control procedures in use.
Before selecting a non-metallic coating thickness gauge, it is important to identify the substrate material and the condition of the coating being inspected. For cured steel, magnetic measurement methods are generally preferred. For aluminum and other non-ferrous metals, eddy current methods should be considered. For wood, MDF, plastic, or other non-metallic substrates, ultrasonic measurement is a suitable option