MIG welding aluminum is possible, but it requires aluminum-specific preparation and controlled heat input. Aluminum conducts heat quickly, forms an oxide layer on its surface, and can distort or burn through when setup or travel speed is unsuitable.
For a more stable weld, clean the joint thoroughly, select compatible wire and shielding gas, and use a forward push technique. The welding source and process should also suit the workpiece thickness and welding conditions.
Summary: Aluminum can be welded with MIG equipment fitted and set up for aluminum. Clean oxide and contaminants before welding. Pure argon is a common shielding-gas choice. Fast travel and controlled heat help limit burn-through and distortion.
Can a MIG welder be used to weld aluminum?
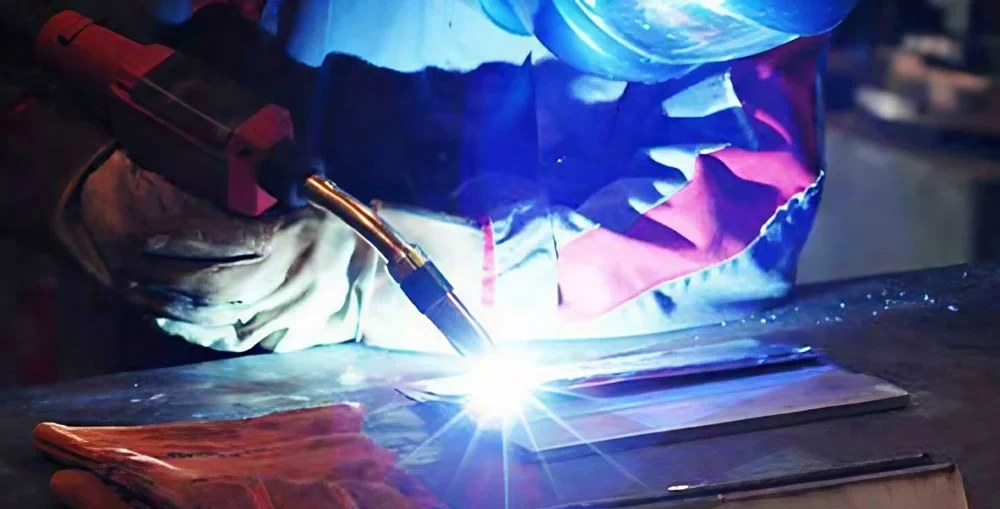
Yes, a MIG welder can weld aluminum when it is prepared with suitable aluminum welding accessories, wire, and shielding gas. MIG welding feeds a consumable wire automatically into the weld while shielding gas protects the weld area from air.
This process is described as fast to operate and suitable for larger or longer components. However, welding aluminum successfully depends on more than the machine itself: joint cleanliness, wire delivery, heat settings, and torch movement all affect the result.
Why is MIG welding aluminum more challenging than welding steel?
Aluminum transfers heat rapidly, has a surface oxide layer, and is prone to heat-related distortion. These properties make heat control and surface preparation particularly important during MIG welding.
| Aluminum characteristic | Effect on the MIG welding process |
|---|---|
| High thermal conductivity | Heat dissipates quickly, so stable and sufficient welding current is needed. |
| Surface oxide layer | Oxide or contamination left on the joint can lead to an impure and weaker weld. |
| Susceptibility to distortion | Excessive or prolonged heat can contribute to warping, especially when travel is slow. |
The source material notes that aluminum oxide melts at about 3,700°F, while aluminum itself melts below 1,200°F. This difference is why removing the oxide layer before welding is essential to controlling the weld.
How should aluminum be cleaned before MIG welding?
Clean aluminum by removing oxide, oil, dirt, and any residue from prior cutting or fabrication. A stainless-steel brush reserved for aluminum can be used to brush in one direction with moderate pressure.
Do not use a brush that has previously been used on steel or stainless steel, because it can introduce cross-contamination. If chemicals or solvents are used, remove them fully before welding; the source recommends a cleaner that does not contain hydrocarbons for oil and similar contaminants.
Should aluminum be preheated before MIG welding?
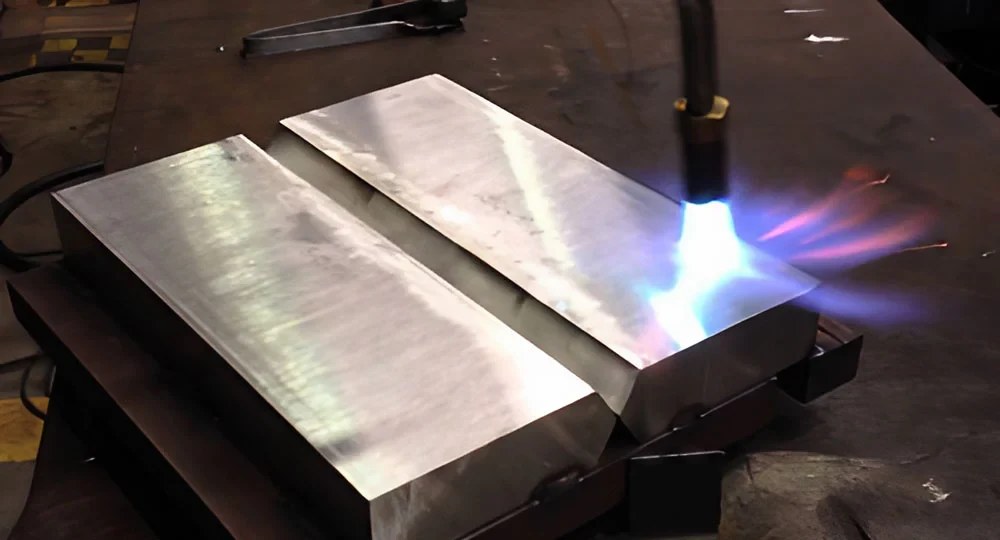
Preheating may be used to help reduce the risk of weld cracking, particularly when joining a thick component to a thin one. In that situation, preheating the thicker component can help balance heat across the joint.
The provided guidance limits preheat temperature to no more than 230°F and recommends using a thermometer for control. Heat should be monitored carefully because aluminum can burn through or distort if too much heat is concentrated in one area.
What torch technique and travel speed are recommended for aluminum MIG welding?
A forward push technique is recommended rather than pulling the torch backward. Pushing the torch can improve cleaning at the weld area, reduce contamination entering the weld, and help the shielding gas cover the weld pool.
Aluminum welding is described as requiring a “hot and fast” approach: current and voltage are generally set higher than for steel, while the torch moves quickly enough to avoid concentrating heat. Slow movement or excessive dwell can cause burn-through and distortion, especially on thin material.
Which shielding gas and wire are used for MIG welding aluminum?
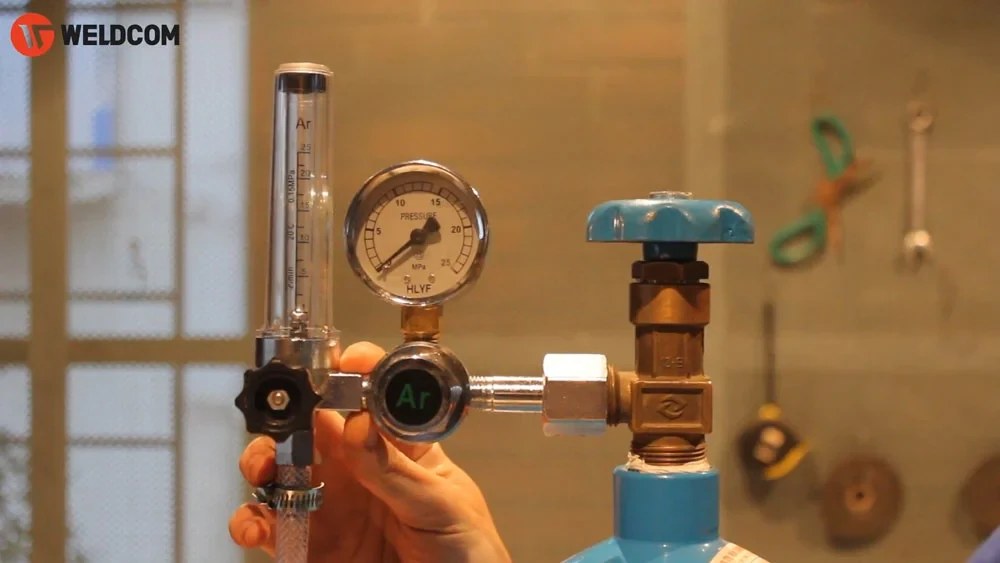
Pure 100% argon is identified as a common shielding gas for aluminum MIG welding. For 5XXX-series aluminum alloys, an argon and helium mixture with up to 75% helium may be used to limit magnesium oxide formation.
Select welding wire with a melting temperature similar to that of the base aluminum to make arc control easier. For thin workpieces, the source specifies 0.8 mm wire used with pulsed welding at a travel rate of 100–300 inches per minute.
What weld profile is preferred when MIG welding aluminum?
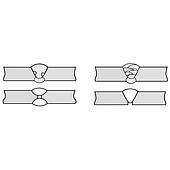
A slightly convex weld profile is preferred because aluminum has a high coefficient of thermal expansion. A concave weld can shrink and tear as it cools, increasing the likelihood of cracking.
Heat input still needs to be controlled: building excessive weld metal is not a substitute for proper settings, travel speed, and preparation. The aim is a lightly convex bead formed under stable conditions.
Which MIG welding modes are mentioned for aluminum?
Spray transfer or pulsed arc methods are recommended options for MIG welding machine. The source identifies constant voltage (CV) for spray-arc welding and constant current (CC) for thick aluminum work requiring more than 350 A.
These modes should be matched to the thickness and welding requirement rather than selected as a universal setting. A stable arc also depends on compatible wire and an unobstructed wire-feed path.
How can common aluminum MIG welding defects be addressed?
Burn-through, cracking, oxide contamination, porosity, and an unstable arc are common problems associated with unsuitable heat control, inadequate cleaning, poor gas coverage, or incompatible wire-feed conditions.
| Welding issue | Likely cause stated in the source | Suggested response |
|---|---|---|
| Burn-through | Heat input is too high or travel is too slow. | Reduce current, increase travel speed, and consider pulsed welding with 0.8 mm wire on thin work. |
| Weld cracking | Thermal expansion and shrinkage; a concave bead is more vulnerable. | Control heat input and form a slightly convex weld profile. |
| Oxide or contamination | Oxide, oil, or solvent remains on the aluminum surface. | Use a dedicated stainless-steel brush and remove contaminants before welding. |
| Porosity | Insufficient shielding-gas coverage or hydrocarbon contamination. | Check argon coverage, avoid drafts, and clean the joint. |
| Unstable arc | Unsuitable mode, wire, feed system, or a bent feed path. | Use compatible wire and settings, then inspect and maintain the wire-feed system. |